Aerosol Can Corrosion Part 2: Formulations & Coatings
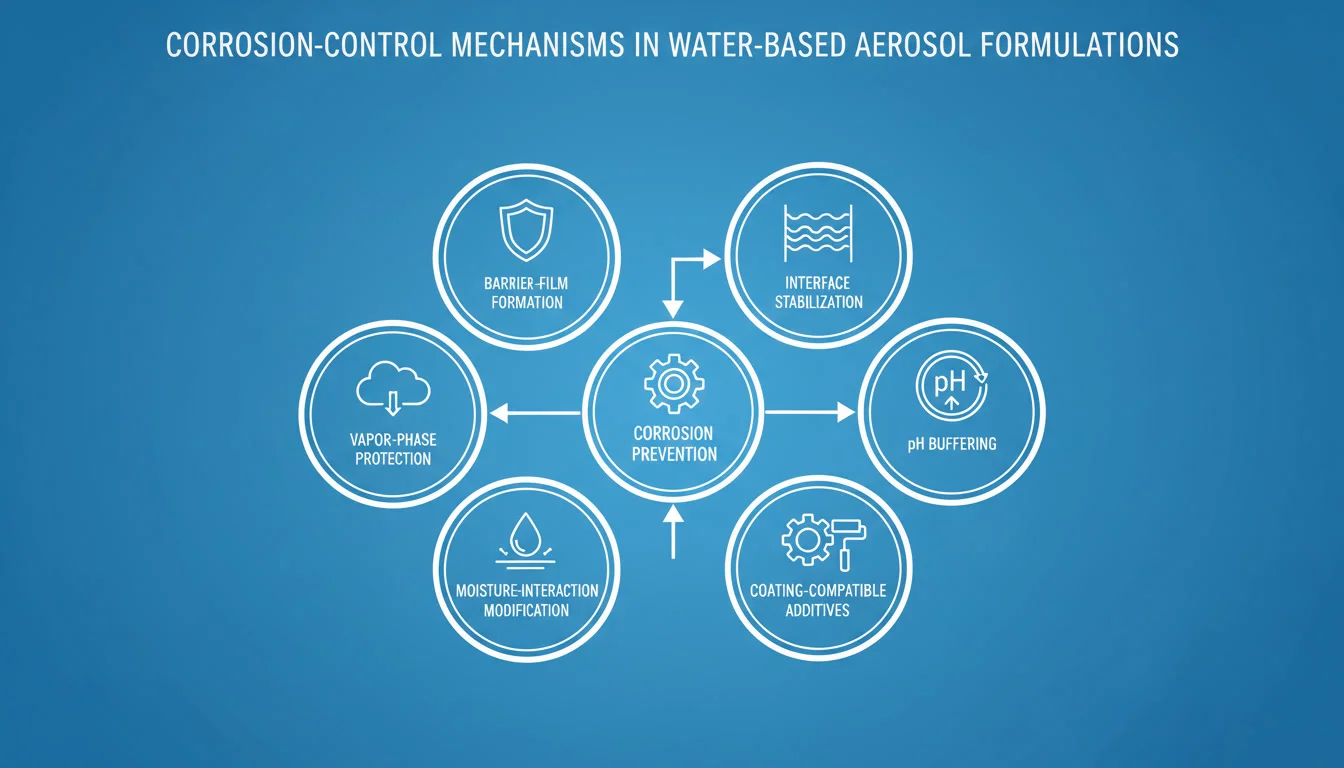
Figure 3: Infographic summarizing formulation-driven corrosion control.
This article examines how formulation components, internal coatings, vapor–liquid interactions, and propellant behavior influence corrosion development inside metal packaging. All explanations provided here are based on established corrosion science and widely documented aerosol engineering behavior, without speculative chemistry.
Guide Contents
- 1. Formulation Influence on Corrosion
- 2. Liquid-Phase Corrosion
- 3. Vapor-Phase Corrosion & Headspace
- 4. Coating Performance & Failure
- 5. Why Coated Cans Corrode
- 6. Propellant & Headspace Interactions
- 7. Analytical & Accelerated Testing
- 8. Formulation Control Approaches
- 9. External References
- 10. Frequently Asked Questions
1. How Formulation Components Influence Internal Corrosion
Water-based formulations introduce a range of interactions that directly influence the corrosion profile of the can. These interactions occur in both the liquid phase and the vapor phase, and are strongly affected by pH, ionic strength, surfactants, solvents, and dissolved gases. The underlying electrochemistry and the container-side factors are covered in Part 1 of this study; this part concentrates on what the formulation itself contributes.
1.1 Water Content and Water Activity
Water activity determines how efficiently ions and gases migrate through the solution. Higher water activity increases electrolyte mobility, which in turn enhances the corrosion rate. Even small increases in available water can accelerate coating penetration and interfacial reactions. This is the same dependence that makes an electrolyte a precondition for galvanic corrosion: without a conductive path, the cell cannot operate.
1.2 Surfactant and Wetting Effects
Figure 1: Surfactant-induced wetting increasing access to coating defects.
Surfactants reduce surface tension and increase wetting. Increased wetting allows the liquid phase to access microscopic coating defects more easily, promoting localized corrosion initiation. This is a well‑documented phenomenon in coating science and metal finishing industries.
1.3 Solvent Polarity and Metal Interaction
Polar solvents change how water interacts with the metal surface and the internal coating. They can alter water penetration rates, influence hydrogen bonding, and modify how quickly the aqueous phase transports ions to exposed metal sites.
1.4 Ionic Impurities and Conductivity Drift
Trace ionic contaminants—introduced through water, raw materials, or filling lines—increase conductivity. Conductivity drift over time correlates directly with higher corrosion current density, especially inside small coating defects.
1.5 pH Drift Over Storage
Water-based formulations often undergo pH drift due to reactions between formulation components and dissolved gases such as CO₂. pH drift destabilizes passive layers and changes the solubility of corrosion products. Both acidic and high-alkaline shifts can initiate or accelerate corrosion processes.
2. Liquid-Phase Corrosion Inside Aerosol Cans
The liquid phase is the most aggressive environment within the package. Corrosion occurs where the liquid directly contacts exposed metal through coating defects such as pores, scratches, thin spots, or regions of incomplete coverage.
2.1 Electrolytic Pathways
In liquid-phase corrosion, water acts as the ion transport medium. Electrochemical reactions occur at anodic and cathodic sites within micro-defects. This behavior is consistent with all metal–water systems across industrial packaging.
2.2 Micro-Environments in Coating Defects
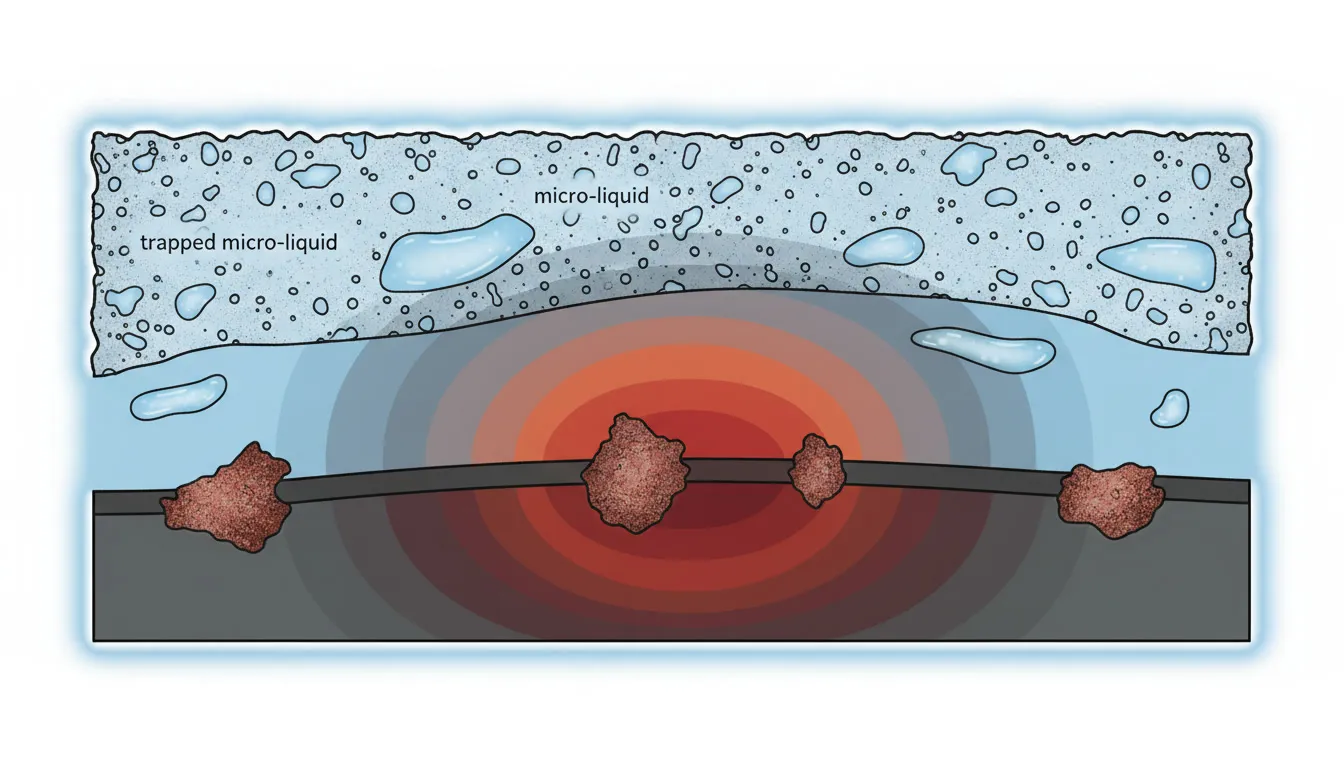
Figure 2: Visual representation of micro-environments inside coating defects.
Within pores and voids, extremely small liquid volumes create micro-environments where oxygen levels, ion concentration, and pH differ from the bulk formulation. These zones promote underfilm corrosion and pitting.
2.3 Liquid Migration and Capillary Action
Capillary forces pull the liquid phase into pinholes, seams, and weld-line irregularities. Once inside, evaporation is limited, and corrosion can proceed unchecked. This is one of the reasons weld lines are highly sensitive in water-based aerosols.
3. Vapor-Phase Corrosion and Headspace Effects
Corrosion does not only occur in the liquid phase. In water-based aerosols, vapor-phase corrosion is equally significant, especially on upper walls, domes, and headspace metal surfaces. The headspace exists because every aerosol needs vapour volume for thermal expansion, as explained in our guide to how aerosol cans work, and perforation of that upper region is one of the routes to the failures catalogued in why aerosol cans leak.
3.1 Condensation Cycles
Temperature fluctuations drive evaporation and condensation cycles inside the can. Condensed moisture forms thin electrolyte films capable of supporting corrosion reactions. This process is well documented in metal can technology and food packaging sectors.
3.2 Distribution of Volatile Components
Volatile formulation components distribute into the headspace and may alter the chemistry of condensed moisture. Vapor-phase chemical behavior is especially important in sprayed products stored in warm environments.
3.3 Vapor-Phase Corrosive Species
Some species can migrate into the vapor phase, influencing corrosion even without bulk liquid contact. Vapor-phase corrosion is a recognized mechanism in pressurized packaging, especially when moisture interacts with dissolved gases.
3.4 Vapor-Phase Protective Mechanisms
Industry uses vapor-phase protective approaches to slow corrosion. These act in the headspace, forming protective molecular layers on exposed metal surfaces. These systems are widely used in metal protection technologies to passivate metal above the solution line.
4. Internal Coating Performance and Failure Modes
Coating choice is constrained by the substrate beneath it, so the tinplate-versus-aluminium decision and the coating decision are made together — the trade-offs are compared in our guide to aluminium versus tinplate aerosol cans.
Internal coatings in aerosol cans are engineered to resist both liquid and vapor-phase corrosion. However, their performance depends on application quality, resin chemistry, thickness, and storage conditions.
4.1 Coating Permeability
All polymeric coatings absorb some amount of water. Absorption increases permeability and eventually allows ions to reach the underlying metal. While slow, this mechanism is unavoidable in long-term storage.
4.2 Hydrolysis and Polymer Breakdown
Water can break down vulnerable chemical bonds in polymer coatings over extended periods. Hydrolysis weakens adhesion, increases porosity, and promotes underfilm corrosion.
4.3 Mechanical Flexing and Pressure Cycles
Internal pressure expands the can slightly. Repeated cycles during temperature variations cause flexing, which can create micro‑cracks in the coating. These cracks expose fresh metal to both the liquid and vapor phases.
4.4 Weld-Line Sensitivity
Welds are metallurgically different from surrounding metal. Coating adhesion over welds is more challenging, and coating thickness may be lower. These factors make weld-lines one of the first areas where corrosion appears.
5. Why Cans Corrode Even When Coated
Polymeric internal linings are highly effective physical barriers, but they are not entirely impermeable to moisture and corrosive gases over years of storage. Electrochemical reactions can still initiate at microscopic voids, weld-seam interfaces, or during periods of high thermal stress. The primary reasons aerosol cans experience corrosion despite having internal protective coatings are outlined below:
- Microscopic voids allow slow electrolyte penetration to the metal substrate.
- Liquid-phase components migrate into polymers over time, weakening adhesion.
- Headspace condensation repeatedly wets upper surfaces, creating galvanic cells.
- Temperature cycling stresses coatings mechanically, creating micro-fractures.
- Formulation pH drift destabilizes the passive layer at the metal–coating interface.
6. Propellant and Headspace Interactions
Propellant choice changes the chemistry the coating and gasket must survive, so it is a corrosion decision as much as a performance one. Our comparison of LPG, DME, HFC, nitrogen and CO₂ sets out the options, and the elastomer side of the same interface is covered in aerosol valve gasket materials.
The propellant contributes to corrosion behavior through its effect on pressure, humidity, solubility, and temperature sensitivity.
6.1 Water–Propellant Partitioning
Water distributes between the liquid phase and the headspace depending on temperature and vapor pressure. This distribution affects how much moisture condenses on the upper can walls.
6.2 Gas Solubility Effects
Dissolved gases influence the baseline electrochemical reactions and can accelerate metal dissolution inside coating defects.
6.3 Diffusion Through Interface Zones
Where liquid and propellant interfaces meet, multi-phase diffusion creates localized chemistry conditions that can favor corrosion of unprotected regions.
7. Analytical and Accelerated Testing Methods
To evaluate the long-term packaging compatibility of new formulations, manufacturers must execute a series of standardized tests. These accelerated testing protocols check the mechanical integrity of the metal can, the adhesion properties of the internal lacquer, and pressure retention over time. Panel-level coating comparisons commonly use the salt spray practice published by ASTM International as B117, while corrosion terminology and test selection follow the standards maintained by ISO. The established analytical methods used to verify container stability include:
- Coating continuity and adhesion testing to verify polymer lining coverage.
- Optical and microscopic inspection of defect propagation on metal surfaces.
- Condensation cycling tests in humidity chambers to evaluate headspace stability.
- Electrochemical corrosion analysis to identify current density pathways.
- Pressure-retention monitoring of filled canisters under accelerated temperatures.
- Weight‑loss and pitting-depth measurements to quantify structural decay.
8. Formulation Approaches for Corrosion Control
While this article does not name specific chemicals, water‑based aerosol corrosion control typically relies on established classes of functional materials. These materials operate through mechanisms documented in corrosion science, such as barrier formation, surface passivation, vapor‑phase protection, and pH stabilization. Each class contributes differently to reducing the interaction between the metal surface and the corrosive environment.
8.1 Barrier‑Film Formers
These materials create a thin, protective film on exposed metal surfaces when present in the liquid phase. The barrier reduces direct contact between the aqueous phase and the metal substrate. Such films slow ion transport, reduce wetting of microscopic defects, and limit access of dissolved oxygen to anodic sites.
8.2 Interface‑Stabilizing Agents
Certain formulation components adsorb onto the metal surface and help stabilize the metal–solution interface. By strengthening the interfacial layer, they reduce electron exchange between the metal and electrolyte. This is a widely recognized mechanism in corrosion science, especially for systems exposed to water.
8.3 Vapor‑Phase Protectants
These are designed to function in the headspace. They migrate into the vapor phase and deposit molecular films on metal surfaces above the liquid line. Vapor‑phase protection is well documented in metal packaging and helps guard upper walls, domes, and vapor‑exposed regions of the can where condensation cycles can initiate corrosion.
8.4 Liquid‑Phase Corrosion Moderators
These components help control the reactivity of the liquid phase by influencing electrochemical behavior, water structuring, or ion mobility. They work within the bulk formulation and inside coating defects, reducing the rate at which anodic and cathodic reactions occur.
8.5 pH Buffering Systems
Stable pH is one of the most important factors in corrosion prevention. Buffering systems maintain the formulation within a controlled pH range over long storage durations. Preventing downward or upward drift helps preserve oxide films and reduces the chance of rapid localized attack.
8.6 Moisture‑Interaction Modifiers
Some formulation components influence water activity, reducing the effective mobility of moisture in the system. Lower water activity reduces electrolyte conductivity and limits the ability of ions to migrate through coating defects.
8.7 Coating‑Compatible Additives
Certain additive classes interact favorably with internal can coatings. They reduce coating permeability, decrease water absorption, or slow hydrolytic degradation. These additives support the long‑term integrity of polymeric linings by maintaining their adhesion and reducing chemical stress at the metal–coating interface.
Together, these formulation strategies act through well‑established metallurgical and electrochemical principles, providing balanced protection across both liquid and vapor phases without relying on any single mechanism.
9. Further Reading & External References
For more detailed technical data and industry-wide protocols regarding corrosion testing and metallic packaging evaluation, refer to the official publications of the following materials science organizations:
Summary
This section expands the corrosion model by focusing on formulation-driven mechanisms. Both liquid-phase and vapor-phase pathways influence corrosion behavior, while coating performance, solvent interactions, pH drift, humidity cycles, and propellant dynamics determine long-term stability. Understanding these mechanisms enables more accurate prediction of failure modes and supports the engineering of robust water-based aerosol products.
Frequently Asked Questions
How does formulation pH affect internal can corrosion?
What is vapour-phase corrosion in an aerosol can?
Why do coated cans still corrode?
Do corrosion inhibitors replace the need for a good coating?
How do propellants influence corrosion behaviour?
What laboratory methods evaluate corrosion before launch?
Troubleshooting Aqueous Aerosol Cans?
Discuss your water-based formulation compatibility and corrosion control strategy with Global Aerosols consultants. Access advanced testing methodologies and stabilizer solutions.
Email: consulting@globalaerosols.com
Website: https://www.globalaerosols.com
Phone: +91 9819548320 +91 8169102990
About the Specialist
Absar Khan is the founder and lead aerosol consultant at Global Aerosols. He possesses cross-disciplinary engineering expertise spanning aerosol corrosion and coating evaluation, formulation compatibility, propellant systems, and regulatory compliance. Absar leads scientific and engineering advisory teams supporting manufacturers globally in technology selection, GMP layouts, validation frameworks, and regulatory strategies.
LinkedIn Portfolio: Connect with Absar Khan on LinkedIn