Corrosion in Water-Based Aerosol Cans: Causes & Control
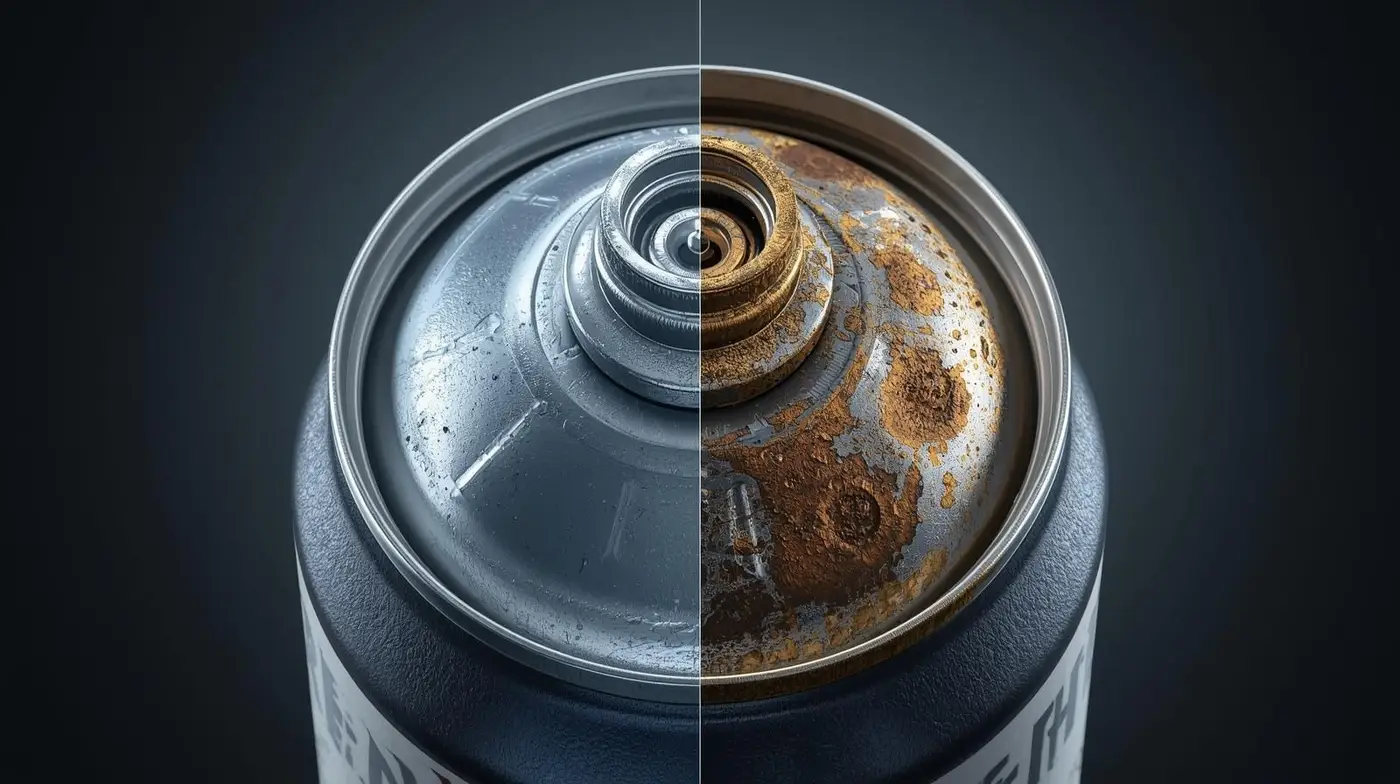
Figure 1: Cutaway cross-section showing corrosion zones inside an aerosol can.
Water-based aerosol systems continue to gain widespread adoption in industrial cleaners, household care, automotive maintenance products, agricultural inputs, and cosmetic sprays. They reduce volatile organic compounds (VOCs), improve environmental compliance, and allow safer handling. However, the presence of water inside a sealed, pressurized metal container changes the corrosion environment dramatically. Water functions as an electrolyte, transports ions, solvates gases, interacts with headspace vapors, and destabilizes protective oxide layers on metal surfaces.
Guide Contents
1. Established Causes of Corrosion in Water-Based Aerosol Cans
The combination of metal, water, pressure, dissolved oxygen, and ionic species makes corrosion the single largest stability challenge for water-based aerosol systems. Understanding the exact, documented mechanisms behind corrosion is critical for manufacturers who want long shelf-life, product integrity, and predictable performance. Below are the primary causes that initiate degradation inside pressurized canisters:
1.1 Water as an Electrolyte
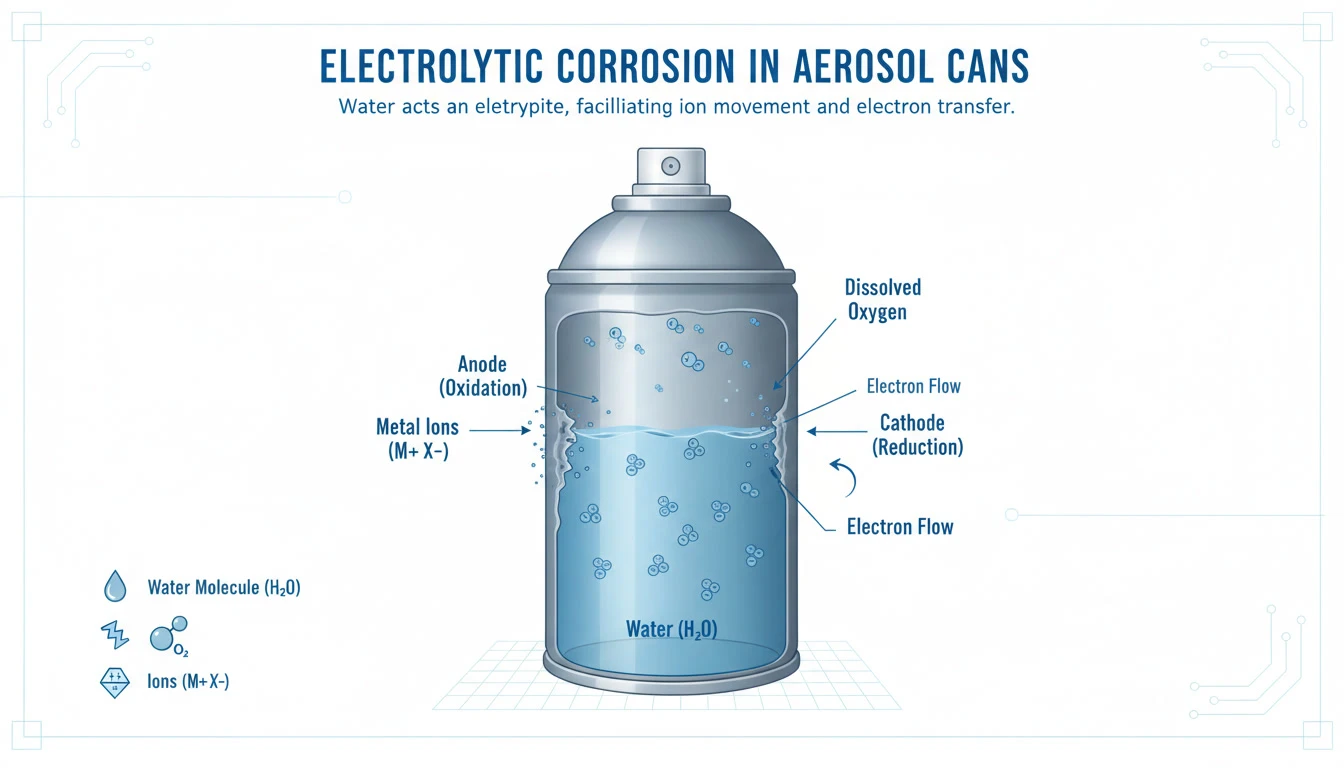
Figure 2: Scientific diagram: water as electrolyte inside aerosol can.
Water dissolves gases and trace contaminants, enabling electron transfer between the metal surface and the surrounding solution. The fundamental corrosion reactions for common can materials are well-established:
Al → Al3+ + 3e- (for aluminum cans)
As electrons move, corresponding reduction reactions occur, forming corrosion products such as iron oxides or aluminum hydroxides. This process begins as soon as water contacts the metal substrate through a defect, weak point, or micro-porosity in the internal coating.
1.2 pH Influence on Metal Dissolution
The chemical stability of the passive oxide film on both steel and aluminum surfaces is highly dependent on the pH of the bulk electrolyte. Extreme acidities or alkalines will dissolve these natural protective layers, leading to direct metal exposure and rapid galvanic dissolution. Extensive corrosion research demonstrates that pH level influences the rate of metal oxidation through the following pathways:
- Acidic pH: Increases metal dissolution by destabilizing the protective films on steel and aluminum.
- Alkaline pH: Promotes dissolution of the natural alumina film on aluminum surfaces.
- Broad pH Swings: Shifts over storage increase the chance of coating delamination and underfilm corrosion.
1.3 Dissolved Oxygen in the Aqueous Phase
Water absorbs oxygen during manufacturing and filling. Oxygen acts as a strong cathodic reactant, accelerating corrosion by accepting electrons released from the metal. The oxygen reduction reaction is a documented driver for corrosion in any water-containing metal package:
1.4 Ionic Species and Conductivity
The presence of ionic contaminants (chlorides, sulfates, nitrates, trace metals) increases conductivity. Higher conductivity directly increases corrosion rate by enhancing current flow through the electrolyte. Chloride ions are especially problematic because they can break down passive films on both steel and aluminum.
1.5 Differential Aeration Cells (DA Cells)
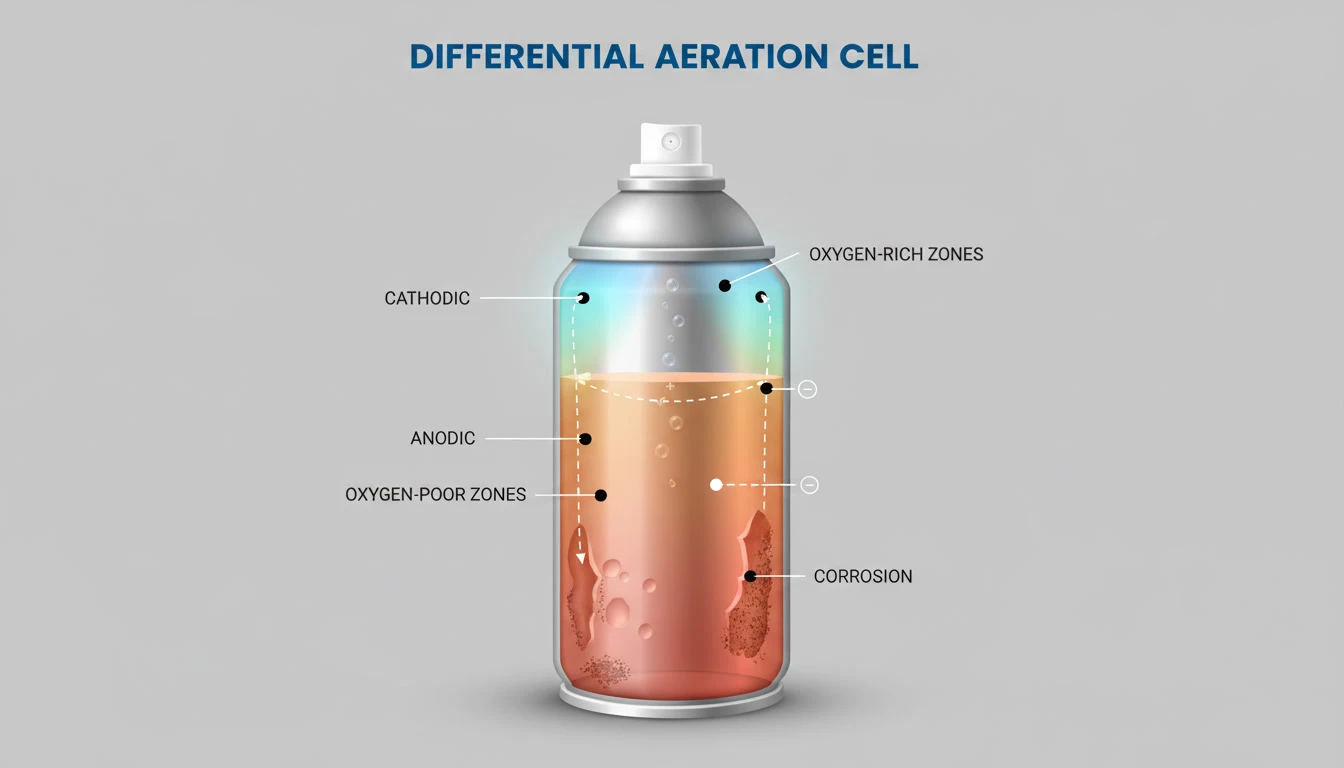
Figure 3: Illustration: differential aeration corrosion mechanism inside can.
Aerosol cans contain geometry variations — weld lines, domes, necks, seams, and curved walls. These features create regions with differing oxygen exposure. Areas with less oxygen become anodic and corrode faster. The differential aeration mechanism is an established principle in corrosion engineering.
1.6 Mechanical Stress & Residual Manufacturing Stress
Aerosol cans operate under internal pressure, producing tensile stress on the walls. Weld seams and necking areas retain residual stress from fabrication. Stress acts synergistically with corrosion to weaken the metal and can contribute to stress-assisted corrosion phenomena.
1.7 Interaction Between Water Phase and Headspace
In water-based cans, the headspace contains a mixture of vaporized water and propellant. Temperature variations create condensation cycles, repeatedly wetting and drying internal surfaces. Wet-dry cycling greatly increases corrosion compared to constant immersion conditions.
2. Types of Corrosion Documented in Metal Aerosol Cans
Corrosion can manifest in several distinct modes depending on formulation properties, package stress, and container coating quality. Identifying the type of corrosion is necessary to execute correct metallurgical and chemical troubleshooting. Below are the six forms of corrosion commonly documented in aerosol plant audits:
2.1 Uniform Corrosion
Occurs when the metal surface reacts evenly across broad areas. It leads to general thinning and reduces burst pressure. Uniform corrosion is predictable but still reduces shelf-life and structural safety margins.
2.2 Pitting Corrosion
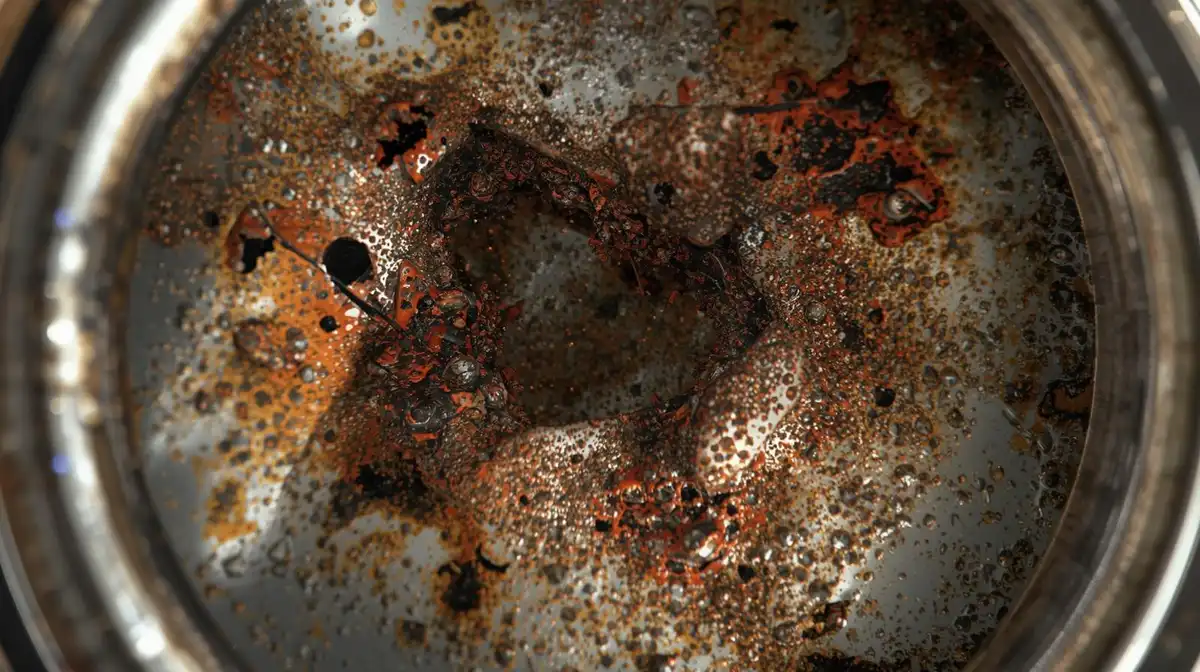
Figure 4: Macro rendering of pitting corrosion in aerosol can wall.
Pitting is the most hazardous corrosion type in aerosol cans. It produces deep, localized cavities that penetrate the metal wall. Pitting often initiates at weld lines, seams, coating pores, scratches, regions with trapped moisture, or areas with chloride accumulation. Pitting can lead to sudden failure even when the rest of the wall appears sound.
2.3 Crevice Corrosion
Develops in shielded areas where oxygen access is restricted, such as under coating defects, at double seams, around the weld bead, or under deposits. Crevices create low-oxygen zones which become anodic, accelerating localized corrosion.
2.4 Stress Corrosion Cracking (SCC)
Occurs when tensile stress combines with a corrosive environment. Water-based systems with certain ionic species create conditions where SCC may initiate in highly stressed zones. SCC causes cracking rather than metal loss, and failures can be sudden and brittle in nature.
2.5 Galvanic Corrosion
If two different metals are in electrical contact while exposed to the same electrolyte, the more active metal corrodes faster. Examples include aluminum bodies in contact with steel components or valve cup contact points. Galvanic corrosion is a well-established mechanism in packaging systems.
2.6 Underfilm Corrosion & Coating Disbondment
Internal protective linings prevent direct metal-water contact. If the coating loses adhesion, moisture penetrates microscopic defects. Underfilm corrosion spreads laterally, lifting the coating and exposing more substrate. This is a leading cause of long-term failure in water-based cans.
3. Industrial Factors That Increase Corrosion Rate
The formulation-side drivers of these mechanisms — inhibitor packages, coating selection and pH control — are treated separately in Part 2 of this study. Corrosion rates are highly dependent on manufacturing practices, storage conditions, and ambient exposure throughout logistics cycles. Standard industrial operations can introduce variables that increase the speed of electrochemical degradation. The primary factors that accelerate internal can failures include:
3.1 Temperature Elevation
Corrosion reactions accelerate with temperature. Pressurized cans stored in hot environments show faster pitting and coating breakdown. Elevated temperatures also increase vapor pressure, affecting headspace dynamics — the same temperature–pressure relationship described in our guide to how aerosol cans work.
3.2 Moisture Cycling
Temperature fluctuations cause condensation in the headspace. Repeated wet-dry cycles are significantly more corrosive than constant exposure because they alternately concentrate and dilute surface ions, promoting localized attack.
3.3 Incomplete Surface Cleaning or Pretreatment
Residual oils, particulates, oxides, and welding residues disrupt coating adhesion and create initiation points. Metal packaging standards worldwide mandate thorough cleaning before coating to reduce corrosion risk.
3.4 Mechanical Damage to Internal Coatings
During transport or filling, cans can deform. Even small dents can crack internal coatings, exposing fresh metal. Handling protocols that minimize denting reduce this failure mode. Where the coating breach sits near the crimp, the resulting attack frequently presents as one of the failure modes catalogued in why aerosol cans leak.
3.5 High Water Activity & High Conductivity
Higher dissolved ions and high-conductivity water allow faster electron flow, accelerating corrosion. Use of low-conductivity water in manufacturing reduces this risk. The same dependence explains why galvanic corrosion requires an electrolyte alongside dissimilar metals in electrical contact: remove the conductive path and the cell cannot operate.
3.6 Lengthy Storage Durations
The longer the product is stored, the greater the chance that pitting will initiate or that pH and other factors will drift. Shelf-life planning must account for long-term corrosion mechanisms.
4. Industrially Established Corrosion Control Measures
Mitigating corrosion requires a multi-barrier approach combining packaging materials engineering, manufacturing controls, and formulation chemistry adjustments. Reliable shelf-life is only achieved when these barriers are designed in unison. Below are the primary industrial mitigation methods employed in modern filling plants:
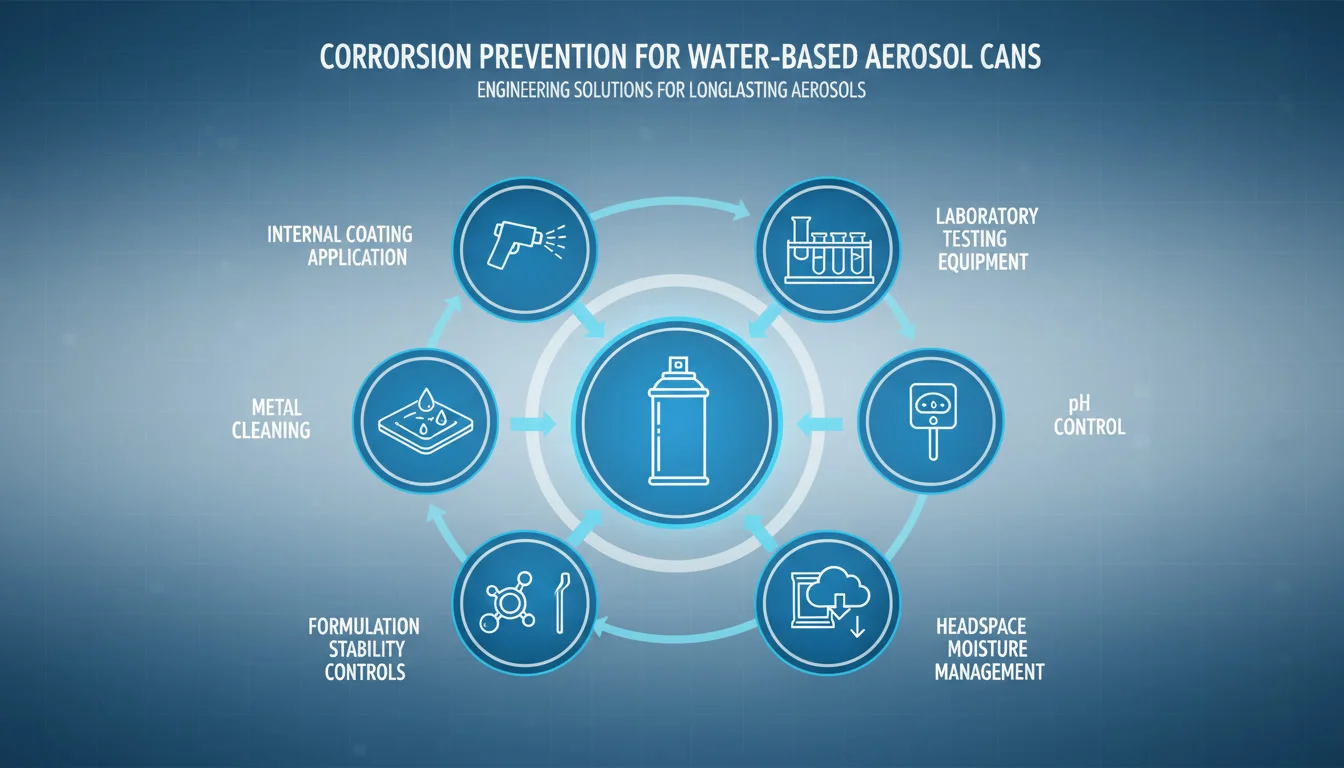
Figure 5: Infographic: corrosion prevention methods for water-based aerosol cans.
4.1 Cleaning, Degreasing & Passivation of Metal Substrate
Proper surface preparation ensures complete removal of contaminants. This step is fundamental in can manufacturing worldwide and is a prerequisite for secure coating adhesion.
4.2 Internal Protective Coatings
Aerosol cans typically use polymeric linings engineered to resist water. These coatings must fully cover weld seams, maintain adhesion under pressure, resist permeation, and withstand wet-dry cycling. Complete coverage is essential—microscopic voids can initiate pitting.
4.3 Control of pH and Water Quality
Maintaining pH in a stable range and minimizing ionic contaminants such as chlorides reduces corrosion rate. Deionized or softened water is commonly used to reduce conductivity. For water-based formulations, check our guide on Household Cleaners Formulations.
4.4 Control of Headspace Conditions
Reducing moisture accumulation in the headspace decreases condensation cycles. Stable storage temperatures and controlled propellant selection reduce the risk of moisture-driven cycling.
4.5 Manufacturing Line Hygiene & Filling Controls
Filling lines must prevent particulate contamination, metal fines, microbial growth (which can alter pH), and ingress of ionic contaminants. Clean manufacturing lines reduce corrosion initiation sites.
4.6 Testing & Quality Evaluation
Common industry tests include burst pressure testing, humidity chamber exposure, cyclic corrosion tests, microscopic inspection of weld seams, coating continuity and adhesion checks, weight-loss tests for general corrosion, and pitting depth measurement using optical microscopy. Accelerated testing identifies corrosion risk early in development.
4.7 Proper Storage & Logistics Management
Cans must be stored at stable temperatures and away from corrosive atmospheres. Avoiding high heat prevents pressure cycling and condensation inside the can. Logistics protocols that minimize mechanical impacts protect coating integrity. Because substrate choice also governs corrosion behaviour, the trade-offs are compared in our guide to aluminium versus tinplate aerosol cans, and the gasket side of the interface is covered in aerosol valve gasket materials.
5. Further Reading & External References
For engineers and formulation scientists seeking deep-dives into corrosion testing standards, specialized technical publications are available from international materials science bodies. These organizations publish peer-reviewed standards and testing protocols for evaluating metal-solution interface reactions. Refer to the following authoritative external resources for global standards:
Frequently Asked Questions
Why are water-based aerosols more prone to corrosion than solvent-based ones?
What role does the internal lacquer play?
How does pH affect corrosion in an aerosol can?
What is crevice corrosion and where does it occur in an aerosol?
How is corrosion resistance tested before launch?
Can corrosion cause an aerosol can to leak or burst?
Facing Corrosion Failures in Aerosol Lines?
Consult with Global Aerosols specialists to analyze your water-based aerosol products. Resolve pitting corrosion, coating disbondment, pH drift, and weld seam failures.
Email: consulting@globalaerosols.com
Website: https://www.globalaerosols.com
Phone: +91 9819548320 +91 8169102990
About the Specialist
Absar Khan is the founder and lead aerosol consultant at Global Aerosols. He possesses cross-disciplinary engineering expertise spanning aerosol corrosion and packaging compatibility, propellant systems, filling line design, and regulatory compliance. Absar leads scientific and engineering advisory teams supporting manufacturers globally in technology selection, GMP layouts, validation frameworks, and regulatory strategies.
LinkedIn Portfolio: Connect with Absar Khan on LinkedIn