Aerosol Fill Weight & Headspace Optimization for Consistent Performance
Aerosol fill weight optimization is the process of setting and controlling how much product and propellant go into each can so that internal pressure, spray performance, and labeled net content all stay within their required ranges. It works by balancing the volume of liquid product against the headspace left for propellant vapor, since that headspace directly determines how much internal pressure the can will reach across its expected temperature range. This matters for aerosol manufacturers because a fill weight and headspace specification that looks correct on paper can still produce pressure failures, inconsistent spray performance, or regulatory net-content violations if it is not validated against real filling line tolerances and worst-case storage temperatures.
What Fill Weight and Headspace Mean
Fill weight refers to the total weight of product concentrate and propellant dispensed into an aerosol can during manufacturing, while headspace is the remaining empty volume inside the sealed can above the liquid fill level, occupied by propellant vapor or compressed gas. These two figures are directly linked — for a can of fixed internal volume, increasing fill weight reduces headspace, and reducing fill weight increases it. Getting this relationship right is a core engineering task in aerosol production, not a simple dosing question, because headspace behaves according to gas physics that determine whether the finished can is safe, functional, and consistent from the first spray to the last.
- Fill weight: Total mass of concentrate plus propellant added to each can
- Headspace: Empty internal volume left for propellant vapor or compressed gas above the liquid fill
- Can internal volume: Fixed by can size and construction, so fill weight and headspace are inversely related
- Target range: Both are set with an upper and lower control limit, not a single exact number
Because fill weight and headspace decisions are made early in the production process and are difficult to correct after crimping, they are typically finalized during formulation development and validated again during scale-up, a transition covered in detail in our Aerosol Manufacturing 101 guide.
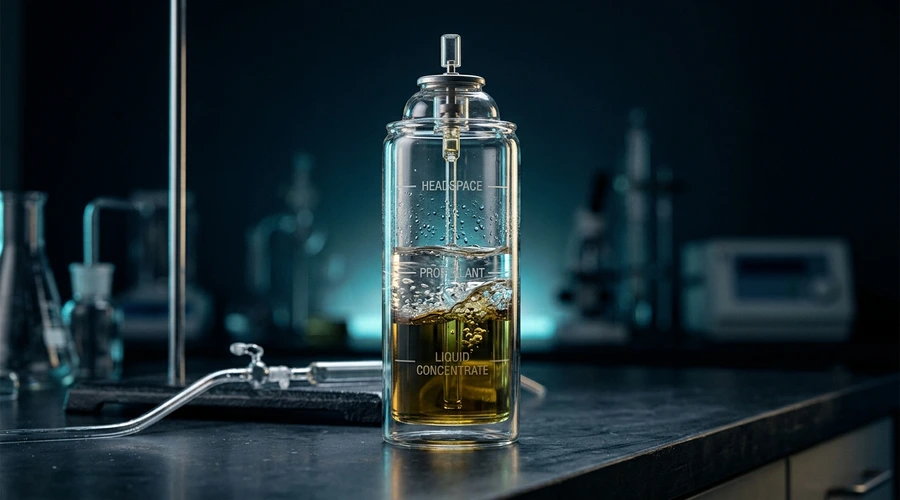
Cross-section view of an aerosol can showing the liquid fill level and the headspace reserved above it for propellant vapor.
Why Headspace Governs Internal Pressure
Internal can pressure is a function of headspace volume, propellant type, and temperature, and understanding this relationship is central to setting a safe fill specification. In a liquefied gas system such as an LPG or DME propellant, pressure remains relatively stable as long as some liquid propellant phase is present, because the liquid continuously replenishes the vapor phase as it is consumed — but reducing headspace still reduces the thermal expansion room available, which becomes critical at elevated temperature. In a compressed gas system using nitrogen or carbon dioxide, headspace volume has an even more direct effect, since compressed gas pressure follows general gas law behavior and changes continuously as headspace volume changes.
This is why aerosol pressure testing protocols specify elevated test temperatures rather than relying on ambient measurements. For a deeper look at how these tests are structured, see our guide on vapor pressure measurement test methods, which explains the standard temperature points used to validate a can's pressure margin.
Calculating a Headspace Target
Setting an initial headspace target starts with the propellant's vapor pressure data at the maximum expected storage temperature — available from sources such as the NIST WebBook thermodynamic database for common hydrocarbon and compressed gas propellants — cross-referenced against the aerosol can's rated proof and burst pressure from its manufacturer specification. Formulators build in a safety margin between the calculated maximum internal pressure at worst-case temperature and the can's rated pressure limits, since manufacturing variation, propellant blend tolerance, and filling equipment accuracy all introduce some variability around the target fill weight.
| Propellant System | Headspace Sensitivity | Primary Design Consideration |
|---|---|---|
| Liquefied gas (LPG, DME) | Moderate — pressure stable while liquid phase remains | Thermal expansion margin at elevated storage temperature |
| Compressed gas (N₂, CO₂) | High — pressure follows headspace volume directly | End-of-life spray performance as gas depletes |
| Bag-on-valve systems | Low direct sensitivity — propellant isolated from product | Propellant chamber volume sized independently of product fill |
Early-stage headspace calculations from vapor pressure data are a useful starting estimate, but they must be confirmed with actual filled samples tested across the intended temperature range before a specification is finalized for commercial production, since dimensional tolerances in real cans and valves introduce variation that a theoretical calculation cannot fully capture.
Weight-Check Methods on the Filling Line
Verifying that each can meets its fill weight specification is typically handled through in-line automated checkweighing immediately after the gassing step, where scales weigh each can (or a statistically representative sample) and compare the result against upper and lower control limits derived from the target fill weight. Fill weight is closely tied to the aerosol fill test methodology described in ASTM D3925, a recognized standard covering the sampling and testing of aerosol products for fill weight and related quality attributes. Cans falling outside tolerance are automatically rejected or flagged for manual review, and control limit breaches are logged for quality trend analysis rather than treated as isolated events.
- 100% in-line checkweighing: Every can weighed automatically as it exits the gassing station
- Statistical sampling: A defined percentage of cans weighed periodically against control limits
- Bench-scale calibration checks: Manual verification against calibrated reference weights to confirm in-line scale accuracy
- Trend monitoring: Control charts tracking fill weight drift over a production run to catch gradual equipment drift before it produces out-of-tolerance cans
For manufacturers evaluating whether to build in-house filling capability or work with a contract filler, weight-check infrastructure and calibration practices are a key differentiator worth assessing directly, a topic explored further in our guide to how contract aerosol filling works.
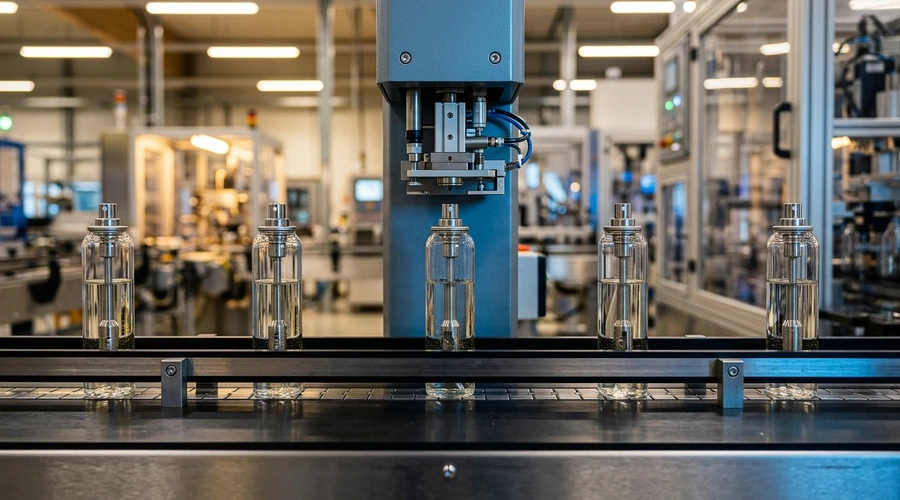
Filling line weight-check station comparing filled aerosol cans against target fill weight control limits before final packaging.
Underfill vs Overfill: Consequences
Overfill and underfill carry meaningfully different risk profiles, and understanding both is necessary to set control limits that are neither dangerously loose nor unnecessarily tight. Overfilling reduces headspace below its design target, which raises the risk that internal pressure at elevated temperature will approach or exceed the can's rated burst pressure — a safety-relevant failure mode, not just a quality defect. Underfilling is generally not a safety risk, but it directly undermines product consistency: a can with less product than intended empties sooner than labeled, and toward the end of its life may show degraded spray characteristics as the ratio of remaining liquid to vapor phase shifts.
- Overfill risk: Reduced headspace, elevated pressure risk at high temperature, potential valve or can failure
- Underfill risk: Reduced usable product, inconsistent end-of-life spray performance, possible net-content labeling violation
- Shared consequence: Both erode consumer trust in product consistency across a batch or between batches
Net content accuracy is also a labeling compliance question in its own right, since declared weight or volume on the label must match what the product actually delivers within an accepted tolerance — a consideration that sits alongside the broader aerosol can safety framework that governs pressure-related risk more broadly.
Maintaining Consistency at Scale
Fill weight consistency becomes harder to maintain as production volume scales, since minor equipment wear, propellant blend variability, and ambient temperature shifts on the factory floor can all introduce small deviations that compound across a long production run. Manufacturers address this by combining tight equipment calibration schedules, statistical process control on fill weight data, and periodic full-batch pressure sampling rather than relying on any single control point in isolation.
The crimping and gassing steps immediately surrounding the fill weight check are themselves sources of variability worth understanding in detail — valve seating quality and gas injection accuracy both interact with fill weight to determine final headspace, which is covered thoroughly in our crimping, gassing, and leak detection guide. Teams should treat fill weight and headspace validation as an ongoing production control discipline rather than a one-time specification set during formulation development, since raw material, equipment, and environmental variables all shift over a product's commercial life. A broader view of how these technology and formulation decisions fit together across the aerosol development process is available in our Aerosol Technology & Formulations resource hub.
Frequently Asked Questions
What is headspace in an aerosol can and why does it matter?
What happens if an aerosol can is overfilled?
What happens if an aerosol can is underfilled?
How is aerosol fill weight checked on a production line?
Does headspace requirement change between propellant types?
How does temperature affect fill weight and headspace decisions?
Is fill weight the same as net content on the label?
Can fill weight and headspace be validated without full-scale production trials?
Need Expert Aerosol Consulting?
Our team provides end-to-end aerosol technical consultancy — from formulation development and propellant selection to filling line setup, regulatory compliance, and market launch strategy.
Get a Free Consultation